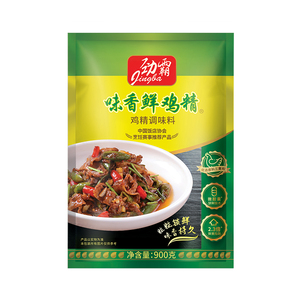
Industrial Chicken Essence Seasoning Powder | Umami Central Kitchen Solution
High-temperature stable umami complex engineered for industrial retort processing, commercial food preparations, and centralized kitchens.

Direct from cGMP, ISO, Halal, and Kosher certified extraction and synthesis manufacturing lines. Tested via HPLC, LC-MS, and enzymatic assays to satisfy global dietary standards.
High-temperature stable umami complex engineered for industrial retort processing, commercial food preparations, and centralized kitchens.
Synergistic multi-mushroom complex (Reishi, Lion's Mane, Chaga, Cordyceps) standardized for β-glucans, triterpenes, and immunomodulatory traits.
Microencapsulated, lyophilized strains showing superior gastric acid and bile tolerance for functional beverages, dairy, and gut health stick-packs.
Enzymatically hydrolyzed marine bioactive peptides with low molecular weight (<1000 Da) for rapid bioavailability and sports recovery nutrition.
Carrier molecule providing supramolecular encapsulation to mask off-notes, boost lipophilic ingredient solubility, and stabilize clear beverages.
Supercritical CO2 extracted botanical rich in citrulline, magnesium, and essential amino acids for cardiovascular wellness and nitric oxide support.
Broken cell-wall green microalgae offering high protein density, natural chlorophyll, and essential minerals for functional detox formulations.
Soluble prebiotic dietary fiber delivering low glycemic impact and selective stimulation of bifidobacteria without compromising formula texture.
A data-informed analysis of regulatory tightening, supply risk mitigation, and consumer-driven clean-label formulation trends across European, North American, and Asia-Pacific markets.
Global CPG formulators are transitioning away from secondary traders to secure audited, direct-from-factory partnerships in China to reduce tariff friction and lead-time volatility.
Global regulatory bodies (EFSA, US FDA, Health Canada) are enforcing strict limits on heavy metals, ethylene oxide (EtO), polycyclic aromatic hydrocarbons (PAHs), and pesticide residues.
Brand owners are eliminating synthetic carriers (e.g., maltodextrin carriers with corn allergens) in favor of organic acacia, native fibers, and green extraction techniques.
Bridging pharmacological extraction standards with shelf-stable food matrices to overcome bio-accessibility limitations and organoleptic challenges.
| Ingredient Domain | Conventional Limitations | Technological Breakthrough | Industrial Target Application |
|---|---|---|---|
| Targeted Peptides (e.g., Tuna Oligopeptides) |
Bitterness, rapid gastro degradation, high molecular dispersion | Controlled multi-stage enzyme cleavage yielding <1000 Da bio-active fractions with high sensory neutrality | Clinical recovery formulations, RTD sports nutrition, anti-fatigue functional shots |
| Active Probiotics (e.g., L. Casei) |
Ambient shelf degradation, cell rupture under stomach pH | Micro-fluidic double-emulsion spray drying and freeze-drying lipid matrix encapsulation | Shelf-stable snack bars, functional ambient beverages, confectionery gummies |
| Hydrophobic Actives (Curcumin, Triterpenes) |
Precipitation, turbidity in beverages, minimal enterocyte uptake | Hydroxypropyl Beta-Cyclodextrin supramolecular inclusion & nano-micellar carrier systems | Transparent functional tonics, sparkling nootropic elixirs, clear nutritional RTDs |
| Botanical Complexes (Mushroom & Herbal) |
Batch variability, low active density, high heavy metal uptake | Bioreactor-controlled mycelial culture and continuous counter-current dynamic extraction | Standardized immune gummies, nootropic coffee blends, adaptogenic capsules |
Operating modern extraction and fermentation centers in China with full analytical substantiation, validated against British, European, and United States Pharmacopeial standards.
Fully closed, continuous SS316 stainless-steel processing networks running automated clean-in-place (CIP) regimens under strict sanitary conditions.
Every lot is released alongside full HPLC/GC-MS chromatography assays, particle size laser diffraction graphs, and verified microbial bioburdens.
Tailored milling to meet exact processing profiles: micronization (up to 200 mesh), agglomeration for instant wettability, and customized bulk density matching.
Full support including SDS, Non-GMO declarations, TSE/BSE free statements, Allergen declarations, and Country of Origin traceability documentation.
Direct technical answers addressing factory auditing, cross-border regulatory compliance, MOQ parameters, and analytical protocols.
Every commercial lot is verified via High-Performance Liquid Chromatography (HPLC) or Ultra-Performance Liquid Chromatography (UPLC) against certified reference standards from USP or European Pharmacopoeia. Certificates of Analysis specify both active percentages and analytical methods to ensure full laboratory replicability.
We routinely support pre-shipment composite sampling directly from production runs, dispatching sealed split-samples to ISO/IEC 17025 accredited laboratories (including Eurofins, SGS, or ALS) for independent validation of pesticides, heavy metals, or active assay content upon contract request.
Yes. We operate commercial jet mills, fluid bed granulators, and cryogenic pulverizers. We can tailor specifications from standard 80 mesh up to 200 mesh superfine powder, or prepare free-flowing dust-free DC (Direct Compression) grades for high-speed tableting and capsule filling lines.
Standard trial MOQs begin at 25 kg fiber drums lined with double pharmaceutical-grade polyethylene bags. Commercial production runs are typically shipped in palletized 500 kg to multi-metric ton ocean consignments. Air-freight orders ship within 5-7 business days, while customized manufacturing campaigns dispatch within 14-21 days.
We provide comprehensive manufacturing flow charts, solvent residual validation (adhering strictly to ICH Q3C limits), full raw material traceability reports, and toxicological evaluation dossiers to support compliance with EU Novel Food, US NDI, and FDA GRAS notifications.
All functional ingredients undergo accelerated (40°C ± 2°C / 75% RH ± 5% RH) and real-time stability studies in accordance with ICH guidelines. Products requiring low humidity or temperature safeguards (e.g., live probiotics, bioactive peptides) are packaged under nitrogen flush into barrier foil laminates with humidity indicators.
Request commercial quotes, batch Certificates of Analysis, or 100g-500g pilot trial samples for formulation testing. Our technical documentation desk returns verification files within one business day.
Send an Inquiry